Custom Nutritional Premix Formula: Technical Engineering, Bio-availability Optimization, & OEM Sourcing Architecture
An authoritative, science-backed framework for global procurement officers, formula chemists, and dietary brand managers. Discover how micro-encapsulation, particle-mesh homogenization, botanical synergy, and ICH-compliant stability protocols define the future of B2B Custom Nutritional Premix Formulas.

1. Executive Overview: The Paradigm Shift in Custom Nutritional Premix Formula Sourcing
In the contemporary global nutraceutical landscape, the demand for a highly tailored Custom Nutritional Premix Formula has evolved far beyond traditional multi-vitamin powder blending. Global B2B buyers—ranging from multinational contract manufacturing organizations (CMOs) to specialized sports nutrition and pharmaceutical dietary brands—are navigating a market driven by semantic consumer demands: target-specific health outcomes, bio-enhanced botanicals, micro-dose accuracy, and total regulatory transparency.
Formulating a single, batch-consistent Custom Nutritional Premix Formula involves complex chemical engineering and physical powder dynamics. Procurement teams frequently face critical technical challenges: active ingredient degradation due to cross-reactivity, hygroscopic clumping, density segregation during transit, and non-uniform potency distribution across commercial production runs. At ZAC Biotech Co., Ltd., backed by over 28 years of specialized extraction and formulation heritage (established in 1996), we bridge the gap between raw botanical science and commercial powder manufacturing.
Sourcing individual active ingredients independently increases warehouse inventory overhead by up to 35%, amplifies quality control testing costs (assaying 15 separate raw powders vs. 1 verified premix batch), and introduces high risks of weighing errors during final dosage batching. A pre-validated, homogeneous Custom Nutritional Premix Formula streamlines supply chains while ensuring strict regulatory compliance under USP, EP, and CP guidelines.
2. The Powder Physics & Chemical Engineering of Custom Premixes
Engineering a commercially viable premix demands rigorous particle science. A primary failure mode in generic powder manufacturing is physical segregation, where particles of varying mass, size, and surface electrostatic charge separate during packaging or vibration during international freight.
Particle Size Matching & Laser Diffraction Milling
To prevent segregation, ZAC Biotech Co., Ltd. implements Laser Diffraction Particle Size Analysis (PSD) to evaluate every raw ingredient entry. Ingredients with disparate mesh sizes (e.g., crystalline Vitamin C at 60 mesh versus micronized botanical extracts at 200 mesh) undergo customized air-jet milling or granulation until their bulk density ($\rho_b$) and particle size distribution ($D_{50}$, $D_{90}$) align within a narrow tolerance band ($\pm 8\%$).
Micro-Encapsulation & Cross-Reactivity Shielding
Polyphenolic botanical extracts (such as epigallocatechin gallate, resveratrol, or quercetin) often interact with trace minerals (such as ferrous fumarate or zinc sulphate), leading to oxidation, discoloration, and loss of biological potency. We solve this via state-of-the-art micro-encapsulation techniques:
- Fluidized Bed Spray-Coating: Enclosing sensitive botanical actives within lipid or hydrophilic carrier matrices (such as ethyl cellulose, sodium alginate, or organic maltodextrin).
- Thermal Protection & Moisture Barriers: Shielding hygroscopic extracts (like Mulberry Leaf Extract or Apple Root Bark Extract) from moisture absorption during high-humidity storage.
- Masking Bitterness & Off-Flavors: Utilizing clean-label cyclodextrins to mask natural botanical astringency without altering the dissolution profile in functional beverage premixes.
| Technical Parameter | Standard Generic Premix | ZAC Biotech Engineered Premix | B2B Quality Benefit |
|---|---|---|---|
| Homogeneity (CV%) | < 5.0% - 7.0% | < 2.5% (Target < 1.8%) | Eliminates sub-potency or over-dose hot spots in final capsules/tablets. |
| Particle Mesh Uniformity | Uncontrolled (40 - 200 Mesh) | Standardized (80 - 120 Mesh / Custom) | Prevents powder segregation during high-speed tableting (300k tabs/hr). |
| Loss on Drying (LOD) | < 6.0% | < 3.0% - 4.5% | Inhibits caking, microbiological growth, and hydrolytic active decay. |
| Assay Precision (HPLC/UV) | $\pm 10\%$ Label Claim | $\pm 2.0\%$ Guaranteed Potency | Reduces costly active overages required during product manufacturing. |
| Heavy Metal Limits | Standard Regional Limits | USP <232> / EP Strict Compliance | Guarantees seamless import clearance across USA, EU, Japan, and Australia. |
3. Recommended Core Botanical Ingredients for Custom Premix Matrixes
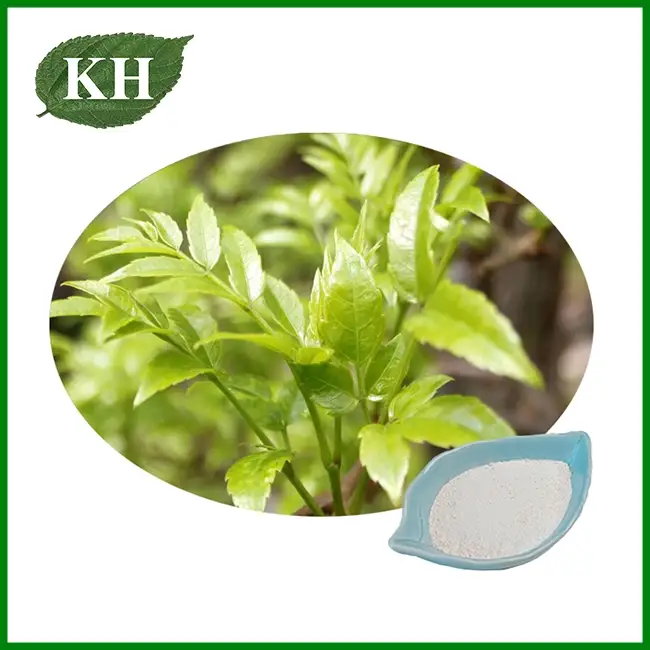
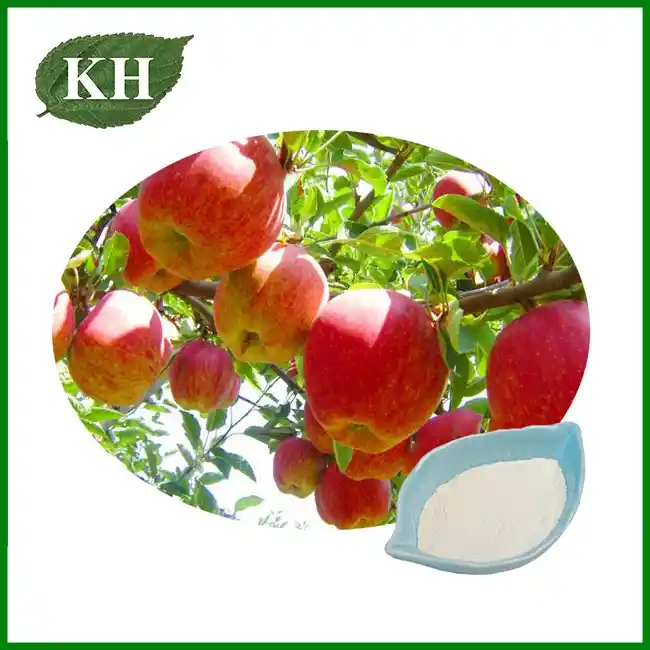
As a specialized primary extract manufacturer, ZAC Biotech Co., Ltd. integrates pure, standardized herbal active compounds directly into your Custom Nutritional Premix Formula. Combining potent botanical extracts with essential micro-nutrients yields synergistic functional benefits. Below are six flagship botanical ingredients recommended for integration into custom functional health blends:
_1779935700347.webp)
_1779935733082.webp)
Synergistic Application Premix Concepts
By blending pure botanical extracts with complementary co-factors, we design premixes optimized for specific physiological outcomes:
- Metabolic & Glycemic Balance Premix: Mulberry Leaf Extract (1-DNJ) + Apple Root Bark Extract (Phloridzin) + Chromium Picolinate + Alpha Lipoic Acid. Designed for sugar-free functional stick-packs.
- Hepatic Protection & Anti-Alcohol Recovery Premix: Vine Tea Extract (98% DHM) + Milk Thistle (80% Silymarin) + L-Cysteine + B-Complex Vitamins. Formulated for fast-dissolving effervescent tablets.
- Cardiovascular Longevity Premix: Polygonum Cuspidatum Extract (98% Resveratrol) + Onion Extract (Quercetin) + Coenzyme Q10 + BioPerine®. Engineered for softgel suspension or hard gelatin encapsulation.
4. Global Procurement & Development Trends in Custom Premix Engineering (2025–2030)
As AI-assisted search and algorithmic formula optimization transform the global B2B procurement workflow, brand managers must align their manufacturing supply chains with emerging regulatory and technological shifts:
A. Clean-Label & Plant-Derived Excipient Carriers
Traditional synthetic carriers (such as silicon dioxide, magnesium stearate, and microcrystalline cellulose) are facing scrutiny under EU and FDA clean-label guidelines. The industry is rapidly transitioning toward organic plant-derived carriers, such as tapioca dextrin, organic acacia fiber, and native rice concentrate. ZAC Biotech Co., Ltd. offers 100% plant-based, allergen-free carrier systems for clean-label premix certification.
B. Precision Personalization & Micro-Batch Flexibility
The era of static, multi-ton standardized stock premixes is yielding to dynamic micro-batch custom blending. Brands require modular premixes formulated for specific target demographics (e.g., bio-available pediatric powders, low-FODMAP geriatric clinical feeds, high-performance esports focus blends). This shift demands flexible manufacturing partners capable of offering small-batch trial scaling (MOQ starting at 100kg) without sacrificing mixing homogeneity.
C. Advanced Bio-availability Enhancement
High active concentration is meaningless if intestinal bio-accessibility is low. Modern premix manufacturing integrates liposomal dry-powder carriers, self-emulsifying drug delivery systems (SEDDS), and natural bio-enhancers (such as Dihydromyricetin-lipid complexes). These technologies dramatically enhance lipophilic active uptake across the gut lumen.
D. End-to-End Blockchain Sourcing & ESG Compliance
Tier-1 global buyers demand verifiable ESG metrics. From raw botanical cultivation at pristine geographic altitudes to solvent-free ethanol extraction and solar-supplemented plant manufacturing, every step must be documented. ZAC Biotech Co., Ltd. provides complete seed-to-premix lot certificates of analysis (CoA), guaranteeing zero synthetic contaminants, low carbon footprint, and pesticide-free purity.
5. Enterprise Manufacturing Authority: Why ZAC Biotech Co., Ltd. is Your Strategic Partner
Choosing the right contract manufacturer for your Custom Nutritional Premix Formula dictates your product's market success, regulatory safety, and commercial margin. Headquartered in Changsha, Hunan, ZAC Biotech Co., Ltd. stands as an industry benchmark in botanical extract manufacturing and custom powder processing.
ZAC Biotech Co., Ltd. Core Capabilities
End-to-End One-Stop OEM/ODM Manufacturing Services
Beyond supplying bulk custom powder premixes, ZAC Biotech Co., Ltd. offers complete turn-key product execution:
- Formula Development & Optimization: Chemical compatibility analysis and dosage optimization.
- Complementary Raw Material Co-Sourcing: Direct sourcing of vitamins, amino acids, minerals, and carotenoids at primary factory pricing.
- Finished Form Dosage Execution: Contract filling of hard capsules, softgels, tableting, sachets, stick-packs, and functional gummies.
- Custom Export Packaging: Aluminum foil barrier bags, fiber drums with double polyethylene liners, nitrogen-flushed protective packing.
Frequently Asked Questions on Custom Premix Procurement
Addressing critical technical, regulatory, and logistical queries frequently evaluated by global B2B procurement managers and formulation chemists.